A visual inspection assesses what the naked eye can observe on the surface of a structure or installation. An NDT inspection goes further: using non-destructive testing techniques, defects hidden beneath the surface are detected without damaging or dismantling the structure. The difference is therefore not one of degree but a fundamental one: the two methods answer different questions about the integrity of an asset. This article discusses when each method applies, which techniques fall under NDT, and how the two methods are combined in practice.
What can and can't a visual inspection detect?
A visual inspection detects visible surface irregularities: corrosion, cracks, paint flaking, contamination, mechanical damage and geometric deformations that can be observed with the naked eye or with simple tools such as a magnifying glass or endoscope. What a visual inspection cannot reveal are internal defects, wall thickness loss behind insulation, subsurface cracking or material fatigue that has not yet manifested itself at the surface.
In practice, a visual inspection is often the first step in an inspection strategy. A trained inspector can use surface symptoms to estimate where further analysis is needed. Blistering in a coating, for example, points to possible corrosion under insulation (CUI). The visual finding then leads to a targeted NDT inspection at that specific location.
The limitations of visual inspection follow accordingly. A pipe can look excellent from the outside while its wall thickness has already been critically reduced by internal corrosion. Welded joints can appear sound on the surface while internal porosity or incomplete penetration is present. In pressurized systems and structures with high safety requirements, a visual inspection is therefore rarely sufficient as the only inspection method.
Which techniques fall under non-destructive testing?
Non-destructive testing (NDT), referred to in Dutch as NDO (niet-destructief onderzoek), covers a wide range of measurement methods used to assess the integrity of a structure or component without damaging the material or dismantling the installation. The most widely used techniques in industrial inspection are:
- Ultrasonic testing (UT): sound waves measure wall thickness and detect internal defects in metal, composites and other materials. Widely used on pipes, tanks and structural components.
- Magnetic particle testing (MT): detects surface and near-surface defects in ferromagnetic materials using magnetic field lines and contrasting particles.
- Penetrant testing (PT): a liquid penetrates open cracks or pores at the surface; after development, defects are made visible. Suitable for metals and non-metals.
- Radiographic testing (RT): X-rays or gamma rays pass through a component and reveal internal defects on a detector or film. Widely used for welded joints.
- Thermographic testing (IRT): infrared cameras detect temperature differences that indicate insulation defects, moisture ingress or irregularities in electrical installations.
- Visual NDT (VT): a structured, documented visual assessment according to standardized procedures also formally falls under NDT; it differs from an informal walk-around through its documented methodology and standardization.
The choice of a specific NDT technique depends on the type of material, the nature of the expected defects, the accessibility of the location and the standards that apply to the installation. In the petrochemical and offshore industries, multiple techniques are often combined to obtain a complete picture of asset integrity.
When is an NDT inspection mandatory or necessary?
An NDT inspection is mandatory when legislation, industry standards or insurance conditions require it, and necessary when safety or business continuity depends on information that a visual inspection cannot provide. In practice, these are the most common situations:
- Pressurized systems: pipes, vessels and tanks covered by the European PED (Pressure Equipment Directive) require periodic NDT inspections as part of legally required inspections.
- Welded joints in structural applications: standards such as EN 1090 for steel structures prescribe NDT on critical welded joints, depending on execution class and load scenario.
- Corrosion under insulation (CUI): insulated pipes and equipment in environments with temperature fluctuations are susceptible to CUI. Because corrosion develops behind the insulation without visible surface signs, targeted NDT inspection is the only reliable method to assess their condition.
- Turnarounds and planned major maintenance: during a plant shutdown, typically once every two to four years in the petrochemical industry, NDT inspections are scheduled to determine the condition of critical components before the installation starts up again.
- After incidents or abnormal operating conditions: after overpressure, temperature excursions, mechanical shock or fire, NDT is necessary to rule out hidden damage before the installation is put back into service.
Beyond legal obligations, risk management plays a decisive role. Asset owners and maintenance engineers use risk-based inspection (RBI) programs in which the inspection frequency and method are tailored to the likelihood of failure and its consequences for safety, the environment and production.
What are the cost and planning differences between the two inspection methods?
A visual inspection is faster and cheaper to carry out: no specialized measuring equipment is needed, the lead time is short and the results are available immediately. An NDT inspection requires certified inspectors, calibrated equipment and sometimes additional safety measures, which increases the direct execution costs. The overall project economics are, however, more nuanced than a comparison of hourly rates alone.
The biggest cost driver in industrial NDT inspections is usually access to the location to be inspected, not the inspection itself. A welded joint at a height of twenty meters or the inside of a tank requires a safe workplace before the inspector can do their work. Traditionally this means scaffolding, which leads to longer lead times, higher material costs and a logistical burden on the site.
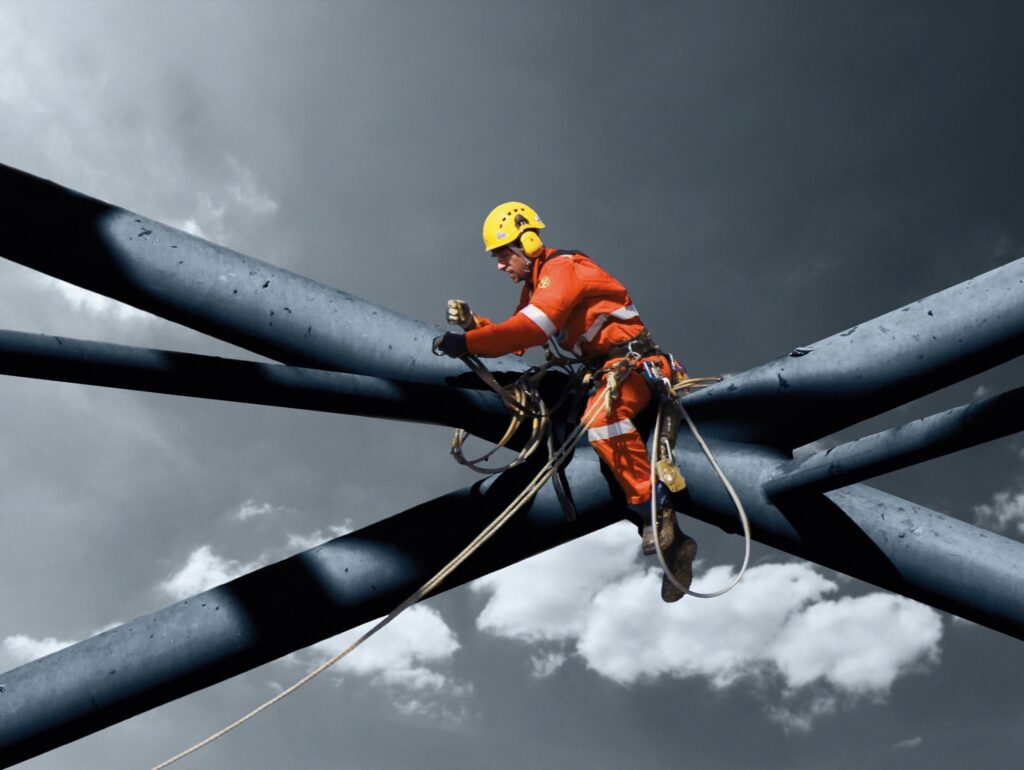
Rope access offers a planning and cost advantage here. A certified rope access team reaches hard-to-access inspection locations without scaffolding, mobilizes quickly and can combine inspection and any repair in the same deployment. That last point is a significant difference: when an NDT inspection identifies a defect, no second mobilization needs to be planned for the repair. The installation can be restarted sooner, which delivers direct production gains.
When comparing planning costs, it also applies that a visual inspection that misses a defect leads to higher costs in the long run: unplanned downtime, emergency mobilization and possibly more extensive repair work. The investment in a targeted NDT inspection at risk-critical locations pays for itself through avoided failures and a longer service life of the installation.
Can NDT and visual inspection be combined in a single site visit?
Yes, and in most industrial inspection programs a combined approach is the standard. A visual inspection is carried out as a first screening: the inspector assesses the entire object and marks locations that require further investigation. Targeted NDT techniques are then applied at those locations. This prevents costly NDT capacity from being deployed on components without cause, while also ensuring that hidden defects are not missed.
The combination is also logistically attractive. When an inspector is already working at height or present in a confined space, it is efficient to bundle visual assessment and NDT measurements into one visit. Every extra mobilization costs time and money, and in production environments every additional site visit means another intervention in the operational planning.
Sky-Access carries out NDT inspections as part of an integrated scope: the same team that reaches the workplace via rope access performs both the visual assessment and the non-destructive measurements, and can proceed directly to repair if a defect is found. This eliminates the traditional split between the inspection party and the executing contractor, which shortens lead times and reduces the coordination burden for the client. More about this approach can be found on the page about Sky-Access as a technical execution partner.
For complex projects in which multiple NDT techniques are combined, for example UT wall thickness measurement combined with visual assessment of the insulation condition and thermographic testing, a detailed inspection program prepared in advance is essential. It records the components to be inspected, the methods to be applied, the acceptance criteria and the reporting requirements. Such a program also forms the basis for the certification and insurance inspection of the installation.
Related Articles
- How to Minimize Downtime in Industrial Maintenance?
- What Does Industrial Maintenance at Height Cost on Average?
- What Are the Most Common Damage Patterns in Wind Turbine Blades?
- How Long Does Maintenance on an Industrial Tank Take on Average?
- Sky-Access at great heights: innovative access solutions for the Euromast in Rotterdam

 NL
 EN